Advanced Gold Extraction Chemicals for the Middle East
Conquering Extreme Desert Heat, Saline Water Kinetics, and VMS Ores
United Chemical supplies guaranteed purity AuCyan™ Sodium Cyanide NaCN (≥98.3%), highly active AuCarb™ Gold Recovery Coconut Shell Activated Carbon (≥99% Hardness), and the eco-compliant AuLeach™ Gold Leaching Agent (GDA) to empower CIP, CIL, CIC, and Heap leaching operations across Saudi Arabia, Oman, Yemen, and the UAE.
The Middle Eastern Mining Landscape: The Arabian-Nubian Shield's Hidden Wealth
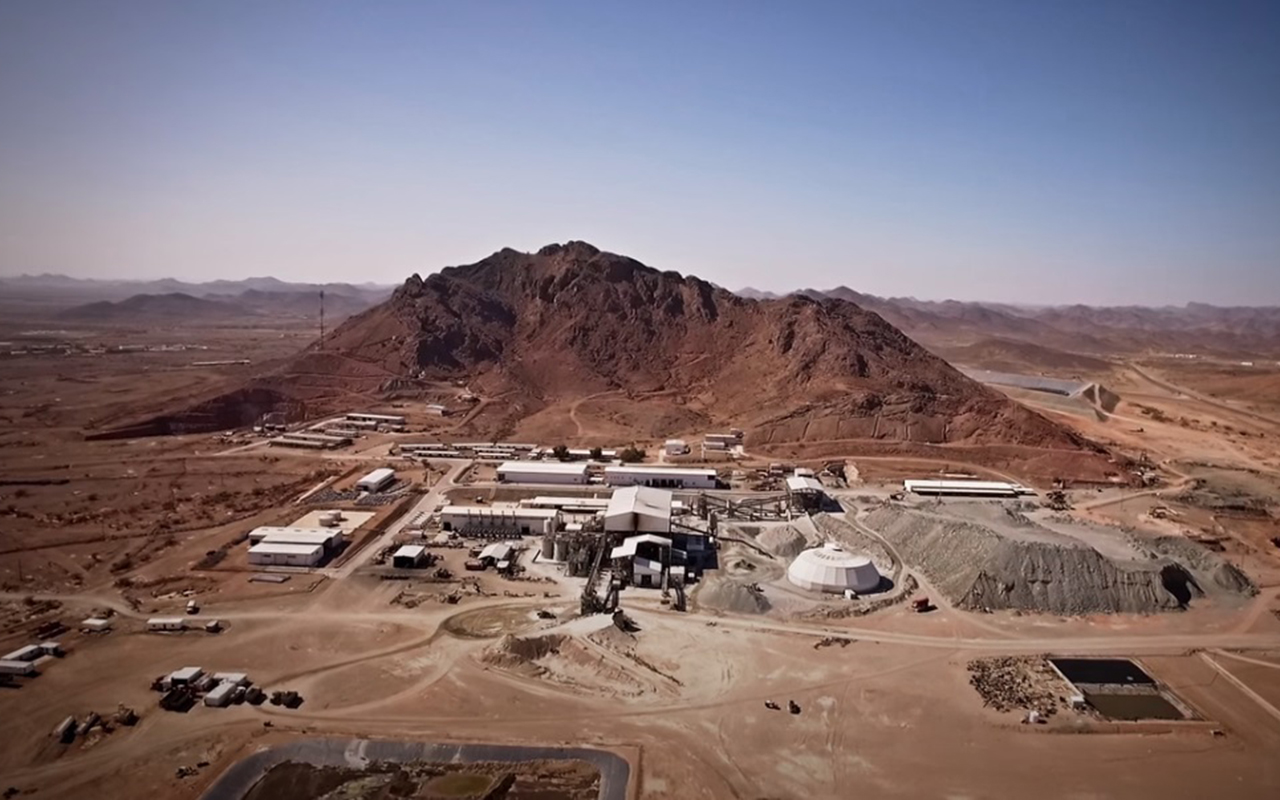
The Middle East is experiencing a massive renaissance in precious metal extraction, driven by economic diversification strategies across Saudi Arabia, Oman, the UAE, and historically rich zones in Yemen. The foundation of this wealth is the Arabian-Nubian Shield, a geological formation famous for Volcanogenic Massive Sulfide (VMS) deposits. However, "Desert Metallurgy" imposes extreme operational penalties. Climatically, ambient temperatures regularly exceed 50°C, requiring exceptional thermal stability for stored chemicals. Chemically, severe water scarcity forces operators to utilize highly saline groundwater or desalinated water, which significantly lowers dissolved oxygen and retards leaching kinetics. Politically, rapid modernization (like Saudi Vision 2030) mandates ultra-strict Environmental, Social, and Governance (ESG) compliance, making toxic chemical transport highly scrutinized.
As an elite manufacturing supplier proudly exporting to 77+ countries worldwide, United Chemical provides Middle Eastern operators with chemical infrastructures specifically engineered to overpower these desert extremes. By offering both ultra-pure conventional cyanidation reagents to conquer high salinity and revolutionary non-hazardous alternatives to bypass complex DG desert logistics, our product matrix fully supports Carbon-in-Pulp (CIP), Carbon-in-Leach (CIL), Carbon-in-Column (CIC), and Heap leaching circuits.
To ensure absolute supply chain security amidst regional geopolitical complexities, we operate entirely via secure maritime ocean freight. We transact under FOB (China ports) or CIF terms directly to vital regional gateways along the Red Sea (Jeddah), the Persian Gulf (Jebel Ali, Dammam), and the Gulf of Oman (Sohar). Backed by a strict Minimum Order Quantity (MOQ) of 1x20' FCL, we deliver factory-direct efficiency straight to the Arabian Peninsula.
1. Conquering Middle Eastern Operational Bottlenecks
Extreme Desert Heat & Chemical Instability
Summer temperatures in the Arabian Peninsula easily surpass 50°C. Standard, poorly packaged Sodium Cyanide can suffer thermal stress and degrade. Reagents require ultra-robust packaging to prevent off-gassing and maintain CN⁻ strength during long desert highway transit.
Highly Saline Process Water
Water scarcity dictates the use of highly saline groundwater or desalinated water. High salinity drastically reduces dissolved oxygen levels and increases scaling risks in Heap Leach networks, severely retarding gold dissolution unless countered by ultra-pure reagents.
Strict ESG Visions & Desert Logistics
National strategies (like Vision 2030) mandate "green mining" practices. Securing permits to transport DG Class 6.1 toxic cyanide across vast, open desert roads is increasingly difficult. A non-hazardous, eco-friendly leaching alternative is rapidly becoming a strategic necessity.
2. The Golden Triangle: United Chemical's Benchmark Solutions
1. AuLeach™ Eco-Friendly Gold Leaching Agent (GDA)
Non-Toxic Chemical (Non-Hazmat)AuLeach™ Gold Leaching Agent (GDA) – The Eco-Friendly Cyanide Substitute
Positioning: A non-toxic leaching agent balancing high recovery yields with strict HSE environmental compliance.
Core Selling Points: General Cargo Export (Non-Hazardous) | Zero Equipment Modification | Superior Yield on Refractory Ores
Faced with increasingly stringent global environmental regulations (HSE), many gold mines face restrictions or bans on cyanide usage. AuLeach™ Eco-Friendly Gold Leaching Agent offers the perfect 100% green replacement for sodium cyanide, aligning "green mining" with high financial returns.
As nations like Saudi Arabia rapidly modernize their mining sectors under Vision 2030, securing environmental permits and managing public perception is paramount. AuLeach™ is officially classified globally as a Non-Hazardous chemical. It clears critical Red Sea and Gulf ports as general cargo, bypassing tedious DG permits. Furthermore, it completely eliminates the catastrophic environmental risk of a toxic chemical spill during long-haul transport across remote, scorching desert highways.
Seamless Direct Drop-in Replacement: Transitioning to AuLeach™ requires zero modification to existing cyanidation equipment (such as Heap Leaching or CIL circuits). It can be directly substituted for Sodium cyanide at 1:1 or recommended ratios to immediately start production.
Non-Toxic Certification & Streamlined Approval (HSE Compliance): Officially certified as a general chemical (Non-Hazmat). This dramatically reduces ocean freight, land logistics, and insurance costs while eliminating tedious toxic chemical permit approvals, cutting mine commissioning lead times by over 50%.
Faster Kinetics & Superior Performance on Refractory Ores: When treating complex, refractory gold ores containing arsenic or sulfur, AuLeach™ exhibits superior resistance to interference and faster leaching kinetics compared to NaCN, frequently achieving a 2% to 5% increase in absolute recovery rate.
Safe Working Environment & ESG Value: Drastically reduces occupational health risks for operational personnel and minimizes environmental contamination hazards, making it the preferred reagent for modern mining companies seeking high ESG ratings.
📊 AuLeach™ Technical Information & Specifications
| Parameter | Units | Guaranteed Specification |
|---|---|---|
| Appearance | - | Solid Powder |
| Operational pH Range | - | 10.5 - 12 |
| Leaching Agent Concentration | % | 30 |
| Standard Packaging | Kgs | Net 25Kgs bag |
Broad Application Spectrum: Highly effective across primary ores, oxide ores, semi-oxide ores, sulfide ores, gold concentrates, and cyanide tailings in both Carbon-in-Pulp and Pool/Vat leaching circuits.
Zero Equipment CAPEX: Fully compatible with existing Heap leaching and CIL infrastructure. Requires absolutely no mechanical retrofitting.
Unrestricted Logistics: Shipped and trucked as general cargo, eliminating the exorbitant costs of hazardous goods import permits and specialized DG escorts across the Arabian Peninsula.
Applicable Metallurgy Processes: Eco-Friendly Heap Leaching, Vat Leaching, CIL / CIP Processing Plants.
2. AuCyan™ Sodium Cyanide (NaCN)
Class 6.1 Dangerous Goods (UN 1689)AuCyan™ Premium Sodium Cyanide ≥98.3; The Industry Standard for Maximum Recovery
Positioning: The performance and purity benchmark for traditional cyanidation in medium-to-large scale gold mining operations.
Core Selling Points: ≥98.3% High Purity | Low Reagent Single-Consumption | Full International Hazmat Compliance
AuCyan™ represents United Chemical's pursuit of perfection in foundational mineral processing chemicals. As the most efficient traditional leaching reagent, we adhere to strict industrial standards to ensure batch-to-batch purity and stability, providing essential momentum for gold mining facilities worldwide. When paired with high-quality activated Carbon, it ensures the most efficient dissolution and capture of gold ions.
Processing gold with highly saline groundwater drastically reduces dissolved oxygen, severely retarding the Elsner dissolution equation. AuCyan™'s extreme ≥98.3% purity ensures an explosive concentration of active CN⁻ ions, chemically compensating for poor oxygenation. Furthermore, its carefully controlled NaOH buffer (≤0.13%) prevents massive calcium scaling in your Heap Leach drip lines when using hard desert water. Its UN-certified steel drums effortlessly withstand the 50°C+ thermal stress of desert storage.
≥98.3% High-Purity Standard: Purity levels far exceeding industry standards guarantee maximum active free cyanide ions (CN⁻) during cyanidation. This drastically accelerates gold/silver dissolution kinetics and maximizes overall leaching efficiency.
Cost-Effective Consumption Control: Ultra-low impurity levels minimize unwanted side-reactions with accompanying minerals (such as copper, iron, and sulfur) in the leaching slurry, significantly lowering reagent consumption per ton of ore processed.
Global-Grade Export Compliance & Delivery: As a regulated dangerous good, supply chain expertise is paramount. United Chemical holds robust UN-certified packaging solutions (steel drums, wooden boxes, Isotanks) and international export qualifications, guaranteeing smooth, safe, and compliant delivery to over 90 gold-producing nations.
📊 Technical Specification: The 98.3% Purity Standard
| Testing Items | Standard (GB/T 19306) | AuCyan™ (Typical) | Operational Impact |
|---|---|---|---|
| Sodium Cyanide (NaCN) | ≥ 98.0% | 98.3% | Maximum gold dissolution kinetics and recovery rates. |
| Sodium Hydroxide (NaOH) | ≤ 0.5% | 0.13% | Superior pH stability; prevents premature hydrolysis. |
| Sodium Carbonate (Na₂CO₃) | ≤ 0.5% | 0.18% | Minimized impurity interference in the leaching solution. |
| Moisture (H₂O) | ≤ 0.9% | 0.3% | Enhanced solid stability during extreme thermal desert storage. |
| Insoluble Substances | ≤ 0.05% | 0.02% | Anti-clogging formula; protects critical pumps and nozzles. |
Applicable Metallurgy Processes: Heap Leaching, Vat Leaching, Carbon-in-Leach (CIL), Carbon-in-Pulp (CIP), Carbon-in-Column (CIC).
3. AuCarb™ Gold Recovery Coconut Shell Activated Carbon
General Cargo (Non-Hazardous)AuCarb™ Gold Recovery Coconut Shell Activated Carbon – Precision Adsorption, Zero Gold Loss
Positioning: Custom-engineered high-strength, high-adsorption coconut carbon tailored for CIP / CIL / CIC gold recovery circuits.
Core Selling Points: Ultra-High Hardness (≥99%) | Rapid Gold-Complex Adsorption Kinetics | High Reactivation Yield
In CIP/CIL processes, Activated Carbon quality directly determines final gold output. AuCarb™ is custom-developed for harsh agitation environments, refined from top-tier Sri Lankan and Southeast Asian Coconut Shells through high-temperature activation and polishing treatments. It is designed to act as the ultimate gold capture matrix, perfectly complimenting our leaching agents.
The Volcanogenic Massive Sulfide (VMS) deposits native to the Arabian-Nubian Shield create extraordinarily dense, heavy, and abrasive slurries in CIL/CIP tanks. The intense mechanical impeller agitation required to mix these heavy pulps will instantly shatter standard activated carbon into fine dust. AuCarb™ provides an elite ≥99% ball-pan hardness, completely eliminating attrition loss and ensuring your gold is securely carried to the elution circuit, not washed into the tailings.
Ultra-High Hardness & Attrition Resistance (Minimal Gold Loss): Mine operators fear carbon attrition in leach tanks leading to gold fines loss. AuCarb™ undergoes special hardening treatment to achieve a hardness rating above ≥99%, completely eliminating costly "gold-bearing carbon" breakdown.
Rapid & High-Capacity Pore Architecture (High Adsorption Kinetics): Gold-cyanide complexes are larger molecular structures. AuCarb™ features a precisely controlled ratio of micro-pores to meso-pores, ensuring rapid entry and firm entrapment of [Au(CN)₂]⁻ complexes with loading capacity far surpassing standard activated carbons.
Extended Service Life & High Reactivation Yield: Following desorption-electrowinning, AuCarb™ recovers over 95% of its original activity after thermal reactivation. It can be recycled through multiple cycles, significantly lowering carbon replacement costs per ton of gold produced.
📊 AuCarb™ Series: Core Parameters Intuitive Comparison Table
| Core Testing Parameter | AuCarb™ BC1100 | AuCarb™ AC50 | AuCarb™ AC55 | AuCarb™ AC60 |
|---|---|---|---|---|
| Market Benchmarking Positioning | Conventional Heap Leach | Comparable: Jacobi G208AS | Comparable: Jacobi G209AS | Advanced: Jacobi G210AS |
| Apparent Density | 0.40 - 0.50 g/ml | 0.48 - 0.55 g/ml | 0.45 - 0.55 g/ml | 0.45 - 0.55 g/ml |
| Ball-pan Hardness | ≥ 98.5% | ≥ 99% | ≥ 99% | ≥ 99% |
| Platelet Content | ≤ 5% | ≤ 5% | ≤ 5% | ≤ 5% |
| Attrition | ≤ 2% | ≤ 1.5% | ≤ 2% | ≤ 2% |
| Total Ash Content | ≤ 5% | ≤ 3% | ≤ 3% | ≤ 3% |
| Moisture | ≤ 10% | ≤ 5% | ≤ 5% | ≤ 5% |
| Adsorption Capacity (K Value) | / | ≥ 26 Kg/t | ≥ 28 Kg/t | ≥ 30 Kg/t |
| Adsorption Rate (R Value) | / | ≥ 50% | ≥ 55% | ≥ 60% |
| Iodine Number | ≥ 1100 mg/g | / | / | / |
| Butane Activity | / | ≥ 19.5% | ≥ 21% | ≥ 23% |
| CTC (Carbon Tetrachloride Activity) | / | ≥ 50% | ≥ 55% | / |
Packing & Shipping: Based on standard 6x12 Mesh or 8x16 Mesh specifications; strictly packed in 25kg heavy-duty laminated elastic PE bags. We offer containerized global shipping under FOB, CIF, CFR terms.
Execution Standards: Complies with American ASTM standards and A.A.R.L. internal mining testing standards. The product has passed third-party inspection and test samples can be provided upon request.
Applicable Metallurgy Processes: Carbon-in-Pulp (CIP), Carbon-in-Leach (CIL), Carbon-in-Column (CIC), Heap Leaching, VAT Leaching.
Validate Performance on Your Middle Eastern Ore Samples
Is highly saline water retarding your kinetics? Are ESG mandates complicating your desert logistics? We invite Metallurgists, Plant Directors, and Supply Chain Managers across the Arabian-Nubian Shield to evaluate our chemical superiority firsthand.
📌 Complimentary Laboratory Sample Availability:
United Chemical proudly provides free laboratory test samples strictly for AuCarb™ Gold Recovery Coconut Shell Activated Carbon and the AuLeach™ Gold Leaching Agent (GDA) - Non-Hazardous. Run comprehensive bottle roll and column tests to verify our kinetic advantages before placing a bulk order.
* Commercial bulk shipments globally commence at a factory Minimum Order Quantity (MOQ) of 1x20' FCL via FOB or CIF maritime terms.
Frequently Asked Questions: Middle Eastern Metallurgy & Logistics
Find clear, expert-driven answers to the most common technical and logistical queries regarding our gold extraction chemicals in the Middle East.
1. How does AuCyan™ perform in highly saline desert process water?
AuCyan™ performs exceptionally well in highly saline water because of its ≥98.3% extreme purity. Saline groundwater inherently holds less dissolved oxygen, which slows down the Elsner dissolution equation. AuCyan™ provides an explosive surplus of active CN⁻ ions that chemically compensates for this lack of oxygen, maintaining rapid leaching kinetics even in harsh desert conditions.
2. Does AuLeach™ support Saudi Arabia's Vision 2030 ESG mining initiatives?
Absolutely. AuLeach™ strongly supports Vision 2030 because it is officially classified globally as a Non-Hazardous chemical. As the Kingdom modernizes its mining sector toward strict "Green Mining" ESG standards, eliminating toxic DG Class 6.1 cyanide from operations secures environmental compliance, protects local groundwater, and drastically simplifies the permitting process.
3. Can AuCyan™ packaging withstand 50°C+ extreme desert heat during storage?
Yes, AuCyan™ is engineered to withstand extreme thermal stress. Our UN-certified 50kg steel drums and 1,000kg reinforced wooden boxes are equipped with heavy-duty, heat-sealed Polyethylene (PE) inner liners. This hermetic seal blocks moisture and prevents chemical breakdown (off-gassing), ensuring complete stability during scorching desert highway transport and on-site storage.
4. Which maritime ports do you utilize for CIF deliveries to the Middle East?
We utilize vital maritime gateways along the Red Sea and Persian Gulf. Key CIF delivery ports include Jeddah Islamic Port (Saudi Arabia), Jebel Ali Port (UAE), King Abdulaziz Port in Dammam, and the Port of Sohar (Oman). This strategic reach ensures secure, compliant import before overland trucking to the mine site.
5. Why is a ≥99% hardness rating critical for activated carbon in VMS ores?
A ≥99% hardness rating prevents activated carbon from being crushed by the dense, heavy slurries generated by Volcanogenic Massive Sulfide (VMS) ores in the Arabian-Nubian Shield. If your carbon is soft, intense impeller agitation will grind it down, carrying your adsorbed gold straight to the tailings dam. AuCarb™'s extreme structural integrity ensures zero attrition loss.
6. How does AuLeach™ GDA solve the risk of transport across remote desert highways?
AuLeach™ mitigates transport risks because it is officially classified globally as a Non-Hazardous chemical. Transporting toxic cyanide across vast, open desert roads carries a severe risk of environmental and public safety disasters in the event of a rollover. AuLeach™ can be safely trucked as general cargo, eliminating this massive liability and the need for heavy security escorts.
7. Are there any capital expenditure (CAPEX) costs to switch to AuLeach™?
There are zero CAPEX costs required because AuLeach™ is engineered as a 100% drop-in replacement. Plant managers do not need to purchase new leaching tanks, alter their Heap leach irrigation systems, or modify their carbon elution circuits. You simply substitute the cyanide with AuLeach™ directly into the process.
8. What types of ores can be processed using the AuLeach™ Non-Hazardous reagent?
AuLeach™ has a very broad application spectrum. According to its Technical Data Sheet, it is highly effective on primary ores, oxide ores, semi-oxide ores, sulfide ores, gold concentrates, and cyanide tailings across both Carbon-in-Pulp and Heap leaching operations.
9. How do metallurgical labs test the concentration of AuLeach™?
Laboratories test AuLeach™ concentration via a standard chemical titration method. This involves using an analytical grade silver nitrate complexing agent and a rhodanine indicator. During titration, the solution changes from yellow to red, and the milliliters of complexing agent consumed precisely indicates the reagent's active concentration.
10. What is the optimal pH range for utilizing AuLeach™ in leaching circuits?
The guaranteed operational pH range for AuLeach™ is between 10.5 and 12. This aligns perfectly with traditional cyanidation circuits, meaning plant operators can continue using standard hydrated lime to manage slurry alkalinity without altering their current procedures.
11. What is the Minimum Order Quantity (MOQ) for exporting to the Middle East?
Our strict Minimum Order Quantity (MOQ) is 1x20' FCL (Full Container Load). This policy applies universally to AuCyan™, AuCarb™, and AuLeach™ to guarantee factory-direct pricing, protect packaging integrity, and optimize maritime freight costs.
12. How does United Chemical guarantee the security of the supply chain?
We guarantee supply chain security by executing all transactions under strict FOB or CIF maritime terms. Operating exclusively with 1x20' FCL minimums and UN-certified packaging, we ensure that the hazardous goods sea freight is handled only by tier-one international shipping lines directly to Red Sea or Persian Gulf ports, passing the inland transport responsibly to the buyer's localized agents.
- Random Content
- Hot content
- Hot review content
- Industry Grade Electron grade 98% Sulfuric Acid H2SO4 Sulphuric Acid Battery Acid Industrial Sulfuric Acid
- T-610 collector Salicyl oxime acid derivative Content 3.5%
- Ferrous Sulfate Industrial Grade 90%
- Toluene
- Fertilizer magnesium sulfate/magnesium sulfate monohydrate
- Sodium sulphate 99% Pharmacy Grade
- Caprylic/capric triglyceride
- 1Discounted Sodium Cyanide (CAS: 143-33-9) for Mining - High Quality & Competitive Pricing
- 2Sodium Cyanide 98.3% CAS 143-33-9 NaCN gold dressing agent Essential for Mining Chemical Industries
- 3China's New Regulations on Sodium Cyanide Exports and Guidance for International Buyers
- 4Sodium Cyanide (CAS: 143-33-9) End user certificate (Chinese and English version)
- 5International Cyanide(Sodium cyanide) Management Code - Gold Mine Acceptance Standards
- 6China factory Sulfuric Acid 98%
- 7Anhydrous Oxalic acid 99.6% Industrial Grade
- 1Sodium Cyanide 98.3% CAS 143-33-9 NaCN gold dressing agent Essential for Mining Chemical Industries
- 2High Purity · Stable Performance · Higher Recovery — sodium cyanide for modern gold leaching
- 3Nutritional Supplements Food Addictive Sarcosine 99% min
- 4United Chemical's Research Team Demonstrates Authority Through Data-Driven Insights
- 5AuCyan™ High-Performance Sodium Cyanide | 98.3% Purity for Global Gold Mining
- 6Digital Electronic Detonator(Delay time 0~ 16000ms)
- 7High-strength, High-precision Shock Tube Detonator
Online message consultation
Add comment: